Industrial Epoxy Flooring in Nairobi
Heavy industrial
Aggregate-filled epoxy mortar screed, 4 to 6 mm · laid in phased bays
Mombasa Road
1,200 m² · phased over nine nights
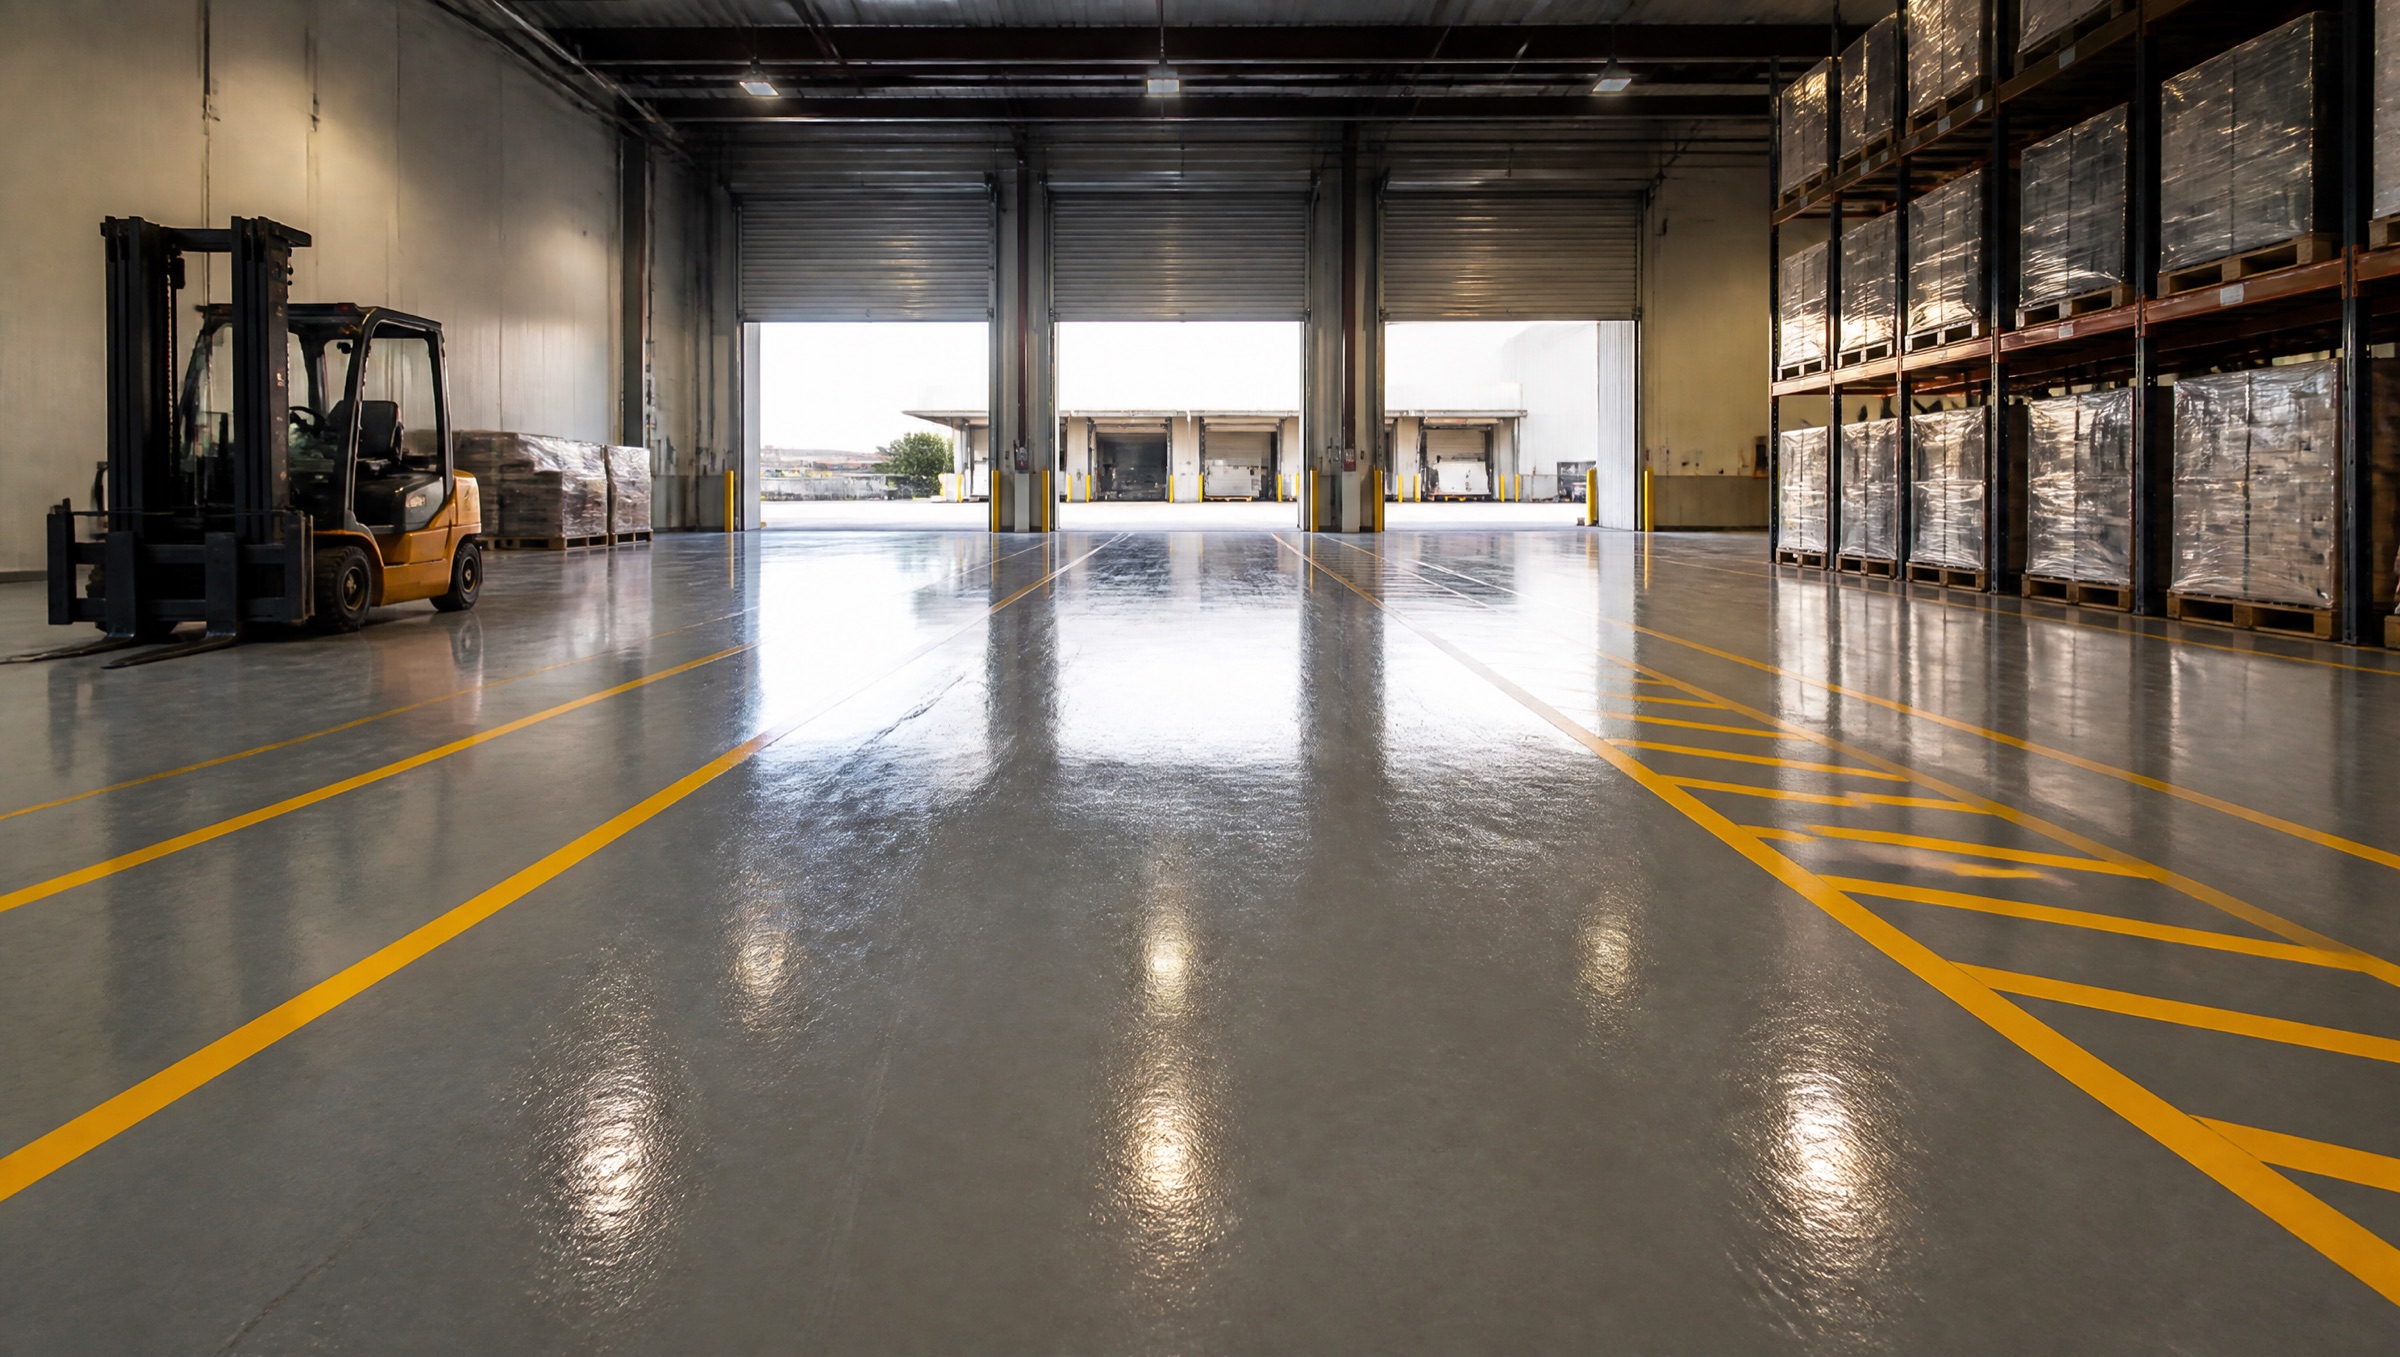
A warehouse floor does not fail across the middle of the slab. It fails in the forklift lane, at the dock edge, and along the joints: the three places where point loads, impact and steel wheels concentrate. So this is not a coating job with thicker paint; it is an aggregate-filled epoxy mortar trowelled on as a screed, specified by what actually runs over it. We lay it in factories, loading docks and go-downs from Nairobi to Mombasa; the floor above is 1,200 m² on Mombasa Road, phased over nine nights.
The thickness bands are trade standard and we hold to them: 2 to 4 mm for light to medium traffic, 4 to 6 mm for general warehouse duty, and 6 to 9 mm where heavy forklifts or steel-wheeled equipment run all day. A good industrial mortar lands somewhere around 8,000 to 12,000 psi in compression; call it 55 to 83 MPa, comfortably above the slab it protects.
Joints are not a detail
The single most common failure we are called to fix on an industrial floor is a coating taken straight across a movement joint. The slab moves, because that is what the joint is for, and the floor splits in a straight line that then spalls under every wheel that crosses it.
Every movement joint is carried up through the system and re-formed, and filled with a semi-rigid filler that supports the joint arris against wheel impact while still allowing the slab to move. Saw-cut control joints that have done their cracking get chased out and filled solid.
Phasing: the floor without the shutdown
Almost nobody can empty a working go-down for a week. We lay these floors in bays, phased around your operation: commonly nights and weekends, one lane or one aisle at a time, with ramped termination edges so a forklift can still cross onto the old floor at the end of a shift.
That is also where line marking gets decided: pedestrian walkways, racking lines, dock edges and hatching, laid into the system rather than painted on afterwards where a wheel can scrub it off. Where chemicals are handled, the bay gets a chemical-resistant topcoat and, if it needs it, a bunded upstand.
Where this system belongs
Specified for
- Forklift lanes and dock edges: the places a standard coating gives up first, and the reason the mortar is specified at all.
- Factory floors and go-downs: pallet traffic, dropped loads and steel wheels, phased so the operation keeps running.
- Chemical handling and battery bays: chemical-resistant topcoat, coved and bunded where spill has to be contained.
Not specified for
- Hot washdown and steam: thermal shock is urethane cement territory (system 03), not epoxy mortar.
- A structurally failing slab: if the concrete underneath is breaking up, a screed on top buys months. We will say so at survey.
- Decorative interiors: this is a work surface. For a floor people look at, see system 01.
- Mortar bed
- 4–6 mm
- Heavy duty
- 6–9 mm
- Compressive
- 55–83 MPa
- Laid
- in phased bays
- Return to use
- 24–72 h
- Joints
- semi-rigid filled
No test, no pour
“Take a coating straight over a movement joint and the slab will draw you a line showing exactly where the joint was.”
Appendix · the build-up
Coat by coat, top coat down to the slab
- Chemical topcoat
- Epoxy mortar
- Moisture primer
- Ground slab
Ground slab
Shot-blasted or ground to an aggressive profile; movement joints identified and carried through the whole system.
CSP 3–5Moisture primer
Heavier film than a domestic primer, because a warehouse slab is rarely a dry one and the screed above is unforgiving.
≈250 µmEpoxy mortar
Resin and graded aggregate trowelled to thickness, ramped out at bay edges so traffic can cross between phases.
4–6 mmJoint re-forming
Every movement joint re-cut and filled with a semi-rigid filler that supports the arris and still lets the slab move.
semi-rigidChemical topcoat
Closes the mortar, with line marking and safety hatching laid into the system rather than painted over it.
per exposure
Living with it
Scrubber-drier with a neutral or mildly alkaline cleaner. Keep the joints clear of debris and have the filler inspected yearly at the dock edge, where impact is worst. Refresh line marking on a planned cycle rather than waiting for it to disappear.